Do You Need ESD Kapton Tape in PCB Assembly?
ESD Kapton tape deserves consideration when unwinding or removing masking tape can expose sensitive components to static charge. But does every PCB masking operation need it? No. The decision depends on the devices present, where tape handling happens, and whether existing controls keep that operation within your ESD program’s limits. This guide explains when to evaluate low-static polyimide tape, when standard tape may remain acceptable, and what buyers should check before approving a replacement.
Is Standard Kapton Tape ESD Safe?
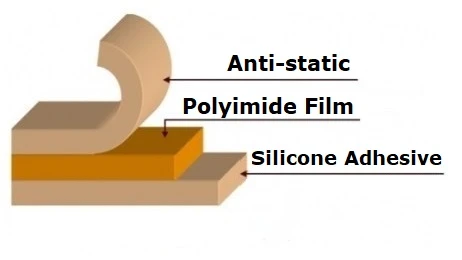
Ordinary polyimide tape should not be assumed to provide ESD protection. Heat resistance and electrical insulation describe different properties from low charging. A tape can protect gold fingers during soldering yet generate charge when peeled away.
For procurement, separate two questions:
- Low charging: How much charge develops during the relevant contact and separation?
- Charge dissipation: Can accumulated charge move away through an effective path?
The EOS/ESD Association’s materials guidance explicitly distinguishes low-charging behavior from resistance measurements. A surface-resistance value alone does not establish unwind or removal performance.
Terms such as “anti-static Kapton tape” and “ESD-safe polyimide tape” therefore need supporting specifications. Ask which surface was tested, by what method, and under what conditions. Avoid approving a material because its label includes “ESD.”
Static During Unwinding, Application and Removal
Tape handling involves contact and separation, often described as triboelectric charging. The EOS/ESD Association’s introduction to ESD explains that materials, separation speed, and humidity can affect charge generation. Your assessment should follow the tape through three steps.
Unwinding: Adhesive separates from the adjacent backing or liner. Check where the dispenser sits relative to exposed assemblies. Moving tape preparation away from boards may reduce exposure, but it does not evaluate later handling.
Application: Inspect the tools, gloves, rollers, and fixtures that contact the tape. A grounded operator does not automatically neutralize charge on an insulating film.
Removal: Test peeling from the actual board surface after processing. A room-temperature result on stainless steel does not establish behavior on solder mask after a thermal cycle.
Removal deserves attention because separation happens at the assembly. Still, do not assume it is always the worst step; compare the actual operations.
When Does PCB Masking Need Low-Static Tape?
Start with the operation, not the board’s appearance. A sparsely populated board can still contain a sensitive device. Conversely, a busy assembly drawing does not by itself prove that every masking step requires ESD tape.
Prioritize evaluation when tape is peeled near exposed sensitive components, applied over electrically connected contact areas, or handled where existing controls are difficult to verify.
| Masking operation | What to investigate before choosing tape |
| Gold finger masking for wave soldering | Removal location, connected circuitry, and charge after the actual heat cycle |
| Connector masking during conformal coating | Component exposure, coating compatibility, and removal conditions |
| Temporary protection during SMT rework | Sensitive devices remaining on the board and how tape is handled nearby |
| Tape preparation at a separate station | Transfer, storage, application, and eventual removal at the assembly |
These are assessment priorities, not automatic pass/fail rules. Ask the ESD coordinator to relate the findings to device sensitivity and the site’s control requirements.
Consider two proposed uses of the same roll: masking a detached metal fixture and peeling tape from contacts on an assembled controller. They need separate assessments even if both pass through the same oven. The useful purchasing question is: “Which operation are we qualifying this grade for?” That keeps an approval from spreading to applications the trial never covered.
The ANSI/ESD S20.20 overview treats process-essential insulators as a risk to assess and control, including through ionization. It does not make purchasing ESD tape a substitute for the control program.
For broader application planning, see our ESD-safe masking guide for SMT and semiconductor manufacturing.
Can You Keep Using Standard Polyimide Tape?
Yes, where a documented assessment supports its use under defined conditions. That might involve an operation without exposed ESD-sensitive items, or a process where verified controls adequately manage the exposure.
Make the approval specific. Record the tape grade, workstation, board family, handling method, and required controls. “Approved for this masking operation” is more useful than “approved for electronics.”
Before retaining standard tape, check three things:
- Exposure: Identify the sensitive items and where charging occurs relative to them.
- Control performance: Verify grounding and, where applicable, ionization at the working position.
- Change triggers: Define when a new device, tape grade, dispenser setting, or process condition requires reassessment.
Production history can support this review, but passing ICT or functional tests alone does not prove ESD control. Equally, unexplained failures should not automatically be blamed on tape. Investigate before assigning a cause.
What Else Changes When You Switch to ESD Tape?
The replacement still has to mask properly. Compare adhesive chemistry, film thickness, total thickness, edge adhesion, and removal after heat exposure.
Check the adhesive first. If downstream bonding or coating restricts silicone, raise that requirement before sampling. Neither “silicone” nor “acrylic” alone establishes temperature suitability or cleanliness. Our silicone versus acrylic polyimide tape comparison explains the selection issues.
For a concrete starting point, River Tape’s K-640 ESD polyimide tape product page lists these silicone-adhesive constructions:
| Published parameter | K-640-60 | K-640-80 |
| Polyimide film thickness | 0.025 mm | 0.050 mm |
| Total tape thickness | 0.060 mm | 0.080 mm |
| Adhesion to steel | 5.5 N/25 mm | 5.5 N/25 mm |
| Surface resistance | 10⁶–10⁹ Ω | 10⁶–10⁹ Ω |
| Listed heat resistance | 260°C | 260°C |
These are published selection values, not an approval for your process. The table does not specify a dwell time at 260°C; confirm exposure duration, cycle count, and test conditions before use. Request grade-specific unwind and removal data where required. Do not convert the resistance range into an assumed peel-voltage limit.
Also, steel adhesion is a comparison value. It does not predict adhesion to your solder mask or coating.
Testing the Tape on Your Boards
Run the candidate alongside the current tape on representative boards or suitable test pieces. Keep width, application pressure, surface preparation, and removal method consistent enough to make the comparison useful.
Agree acceptance criteria before the trial. Otherwise, a clean-looking sample can distract from a missed electrical or handling requirement.
| Trial check | What to record |
| Unwind and application | Dispenser setup, handling position, and feeding consistency |
| Thermal exposure | Actual temperature profile, dwell time, and number of cycles |
| Masking performance | Edge lift, shrinkage, and solder or coating intrusion |
| Removal | Board temperature, peel method, tearing, and visible residue |
| Static assessment | Measurement method, geometry, humidity, and control status |
Have a competent ESD specialist select instruments suited to the measurement. Field strength and surface voltage are different quantities; instrument distance and response also matter. Do not assume a handheld meter captures every brief peak. Our guide to surface resistance versus unwind and removal voltage explains why these results should be reported separately.
Visual inspection is a useful first check for residue. Where electrical contacts or downstream bonding are critical, add the cleanliness or functional checks that the process requires.
Include expected production variation in the trial plan. A slow manual peel in comfortable laboratory humidity may not represent the working station. If the available measurement cannot characterize the operation, record that limitation and arrange a suitable assessment. Treat missing evidence as an open qualification item, rather than quietly interpreting it as a pass.
For purchasing, retain the approved grade and trial record together. Specify width, roll length, film and total thickness, and the documentation needed for repeat supply. Record the sample lot so later complaints can be compared against an identifiable baseline.
Need a sample recommendation? Send the masking location, substrate, thermal profile, removal conditions, ESD requirements, and roll dimensions through our polyimide tape manufacturing and custom-slitting page. Include expected order quantity so the discussion covers both qualification and repeat supply.

FAQ
No. Automation changes how tape is handled; it does not eliminate contact and separation. Evaluate the actual dispenser, its grounding arrangements, contacting materials, and position relative to sensitive assemblies. Include the intended operating settings in the trial instead of relying only on a manually unwound sample.
Potentially, as part of a verified ESD control plan. Ionization can neutralize charge on insulators, but its effectiveness must be checked at the relevant location and under operating conditions. Neither installing an ionizer nor switching to low-static tape automatically establishes that the whole process is controlled.
Preparing strips away from exposed boards can relocate the unwinding step. It does not eliminate charging during pickup, application, or final removal. Assess the complete handling sequence, including any temporary storage surface. Smaller pieces alone are not evidence that a masking operation is acceptable.
Do not treat the labels as interchangeable specifications. Clarify whether the supplier means reduced charge generation, a measured resistance range, or both. Ask for the tested surface and conditions. Two products described as anti-static can provide different evidence for the operation you need to control.
Compare cost per accepted assembly, including tape consumption, masking time, removal labor, and documented rework. Use measured differences from your trial. If an ESD grade costs more, justify it through the control requirement or demonstrated process benefit, rather than an assumed reduction in failures.
Related Articles:
- How to Choose Kapton Tape Thickness for PCB Gold Finger Masking: 1 mil vs 2 mil vs 5 mil
- Kapton Tape for PCB Masking: Edge Lifting, Solder Leakage, and How to Eliminate Failure Risk
- Kapton Tape RFQ Guide: How to Specify the Right Polyimide Tape for PCB Masking Without Costly Misquotes
- Kapton Tape for Conformal Coating Masking: How to Prevent Coating Bleed and Protect Critical PCB Areas