What Buyers Should Check When Choosing an ESD Polyimide Tape Manufacturer
An ESD polyimide tape sample may mask one PCB perfectly and still say little about the next 500 rolls. It could come from another construction, be tested under different humidity or receive more care than routine production. The risk usually appears later—during removal, narrow-roll dispensing or incoming inspection.
Choosing an ESD polyimide tape manufacturer means following one grade from quotation to production lot. Buyers may search for kapton tape manufacturers, but Kapton® is a DuPont trademark. The supplier should identify branded or generic polyimide film accurately; either can then be evaluated on evidence.
The First Check Happens Before the Sample Arrives
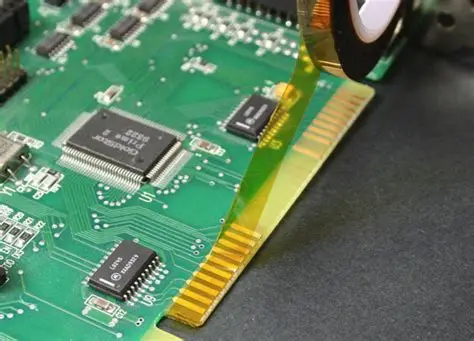
Width and quantity are not enough for recommendation. For PCB gold-finger masking, describe the board finish, masking position, flux, thermal profile, removal point and when exposed ESD-sensitive devices enter the process.
Tape removed after wave solder beside populated boards has a different job from tape used on an unpopulated fixture. The ESD & Semiconductor Masking page helps define the application; use the industrial tape buying guides first if material choice is still open.
Equipment matters too. A technician can work around uneven unwind; an automatic narrow-roll dispenser may misfeed when tension or edge quality drifts. The supplier should know which situation it is quoting.
Make the Quotation, Sample and TDS Describe the Same Tape
Record one construction before comparing prices: product code, film and adhesive types and thicknesses, total thickness, static-control mechanism and side where applicable, liner, roll dimensions, core, winding direction and packaging.
Compare it with the quotation, sample label, TDS and ESD report. Codes should match. “Equivalent grade” needs a written construction comparison. A film or adhesive change made to reach a price target requires review.
River Tape’s ESD polyimide tape configurations illustrate this: 0.025 mm film with 0.06 mm total thickness, and 0.05 mm film with 0.08 mm total thickness, both with silicone adhesive. These are screening data, not automatic order tolerances or release limits.
At receiving, an SQE should be able to place the roll label beside the specification and identify the approved construction without guessing from color.
Surface Resistance Is Only One Part of the ESD Story
A value such as 10⁶–10⁹ Ω needs context: tested side, resistance or resistivity, temperature, humidity, method and whether it is typical data or an acceptance limit.
ANSI/ESD STM11.11-2022 defines equipment, preparation and conditioning for reproducible planar-material measurements. The EOS/ESD Association notes that resistance or resistivity does not necessarily predict low-charging behavior.
The 3M 5419 technical data sheet shows useful reporting practice: it separates charge during roll removal from PWB removal and states 21°C, 50% RH and an ESD-controlled environment. Published values are identified as typical; final specifications are tied to the commercial-product CoA.
Those figures are not universal targets. The useful part is the reporting structure: event, environment, substrate and data status. An ESD tape supplier should provide comparable context where charging matters. See the resistance, unwind and removal voltage guide for the measurement differences.

Put the Temperature Claim Back into the Production Process
“260°C heat resistance” is not a masking window without exposure time, substrate and removal result.
The 3M 7419L data sheet ties its statement to 10 minutes at 260°C and clean removal without staining from copper. It also links its non-silicone adhesive choice to reducing contamination potential before later bonding or conformal coating.
This does not make acrylic universally better than silicone. It shows why the next operation belongs in the brief. On the line, the tape must hold its edge, keep solder or coating out, and remove without tearing, residue or unacceptable charging.
Flux, cleaner, solder mask and board finish can alter results. A credible polyimide tape manufacturer defines what was tested and supports a trial outside that evidence.
Look at the Slit Roll the Way an Operator Will
For custom width polyimide tape, inspect the slit roll: width at several positions, edge nicks or adhesive smear, telescoping, dish, core alignment and deformation. Unwind enough material to notice tension changes as diameter falls.
The 3M 7412B data sheet specifies splice-free maximum length, slit-width tolerance, core dimension and individual packaging. Its values are product-specific, not benchmarks. They show the level of roll information an industrial tape manufacturer can define.
Technical guidance on pressure-sensitive adhesive converting notes that low winding tension can produce telescoping, while excessive tension can squeeze adhesive toward roll edges. Either can disrupt automated feeding.
Agree permitted joints, marking, bags, separators, core support and carton orientation. Bulk polyimide tape must survive converting, export and storage. River Tape’s polyimide tape manufacturer page describes available formats; order tolerances still need written agreement.
Can the Approved Sample Be Reproduced Six Months Later?
A factory audit becomes useful when one finished lot can be followed backward from slit-roll label to converting record, master roll, film and adhesive batches—and forward to retained sample, inspection record and carton.
Separate every-lot checks from periodic and development data. An ESD tape CoA should contain agreed lot-specific results, methods and limits; a copied TDS table is not batch evidence.
Ask how changes to film source, adhesive, static treatment, test method or converting location are notified. For private label polyimide tape, packaging must preserve the underlying factory code and tape lot traceability.
Documents That Procurement and IQC Can Actually Use
Depending on grade and market, the package may include TDS, SDS, RoHS or REACH evidence, material declaration, storage and shelf-life statement, packaging specification, origin and batch report. “Full documents available” is too vague.
Check manufacturer, product code, date, revision and scope. A standard tape report does not cover the ESD grade automatically. Use the Tape Datasheets Download Center for initial review, then control approved project files by revision.
Run the Sample through the Real Process
Use the proposed production width, core and winding—not a hand-cut strip. Apply it to the actual PCB with normal tools, run the full heat and chemical sequence, and remove it at the production point.
Record edge seal, leakage, shrinkage, residue, tearing, removal and relevant ESD results. Retain the approved roll, lot, photographs and record. A second lot adds repeatability evidence for higher-risk programs.
Describe a failure before requesting “more adhesion.” Edge lift, transfer and high removal voltage differ. The ESD tape troubleshooting section helps separate material, process and measurement causes.
Use Pass/Fail Gates Before the Weighted Score
A weighted scorecard is useful only after four gates are passed:
- The quoted grade, sample and technical records identify the same construction.
- Mandatory ESD and compliance requirements have usable evidence.
- The production-representative sample passes the agreed process trial.
- Lot identification and change notification are acceptable.
A supplier failing a gate should not recover through price or lead time. For those that pass, compare grade-specific ESD evidence 25%, process fit 20%, lot and change control 20%, roll quality 15%, documents 10% and commercial terms 10%. These are adjustable, not industry-standard weights.
Score documented evidence: zero for none, three for relevant evidence with gaps and five for current, grade-specific, reproducible evidence. Procurement and engineering should score independently before reconciliation.
A Two-Stage Supplier Review
Before requesting samples, six questions are usually enough:
- Which exact grade matches our application, and what is its complete construction?
- Which ESD results belong to that code, and under what test conditions?
- What thermal process, substrate and removal condition support the heat claim?
- What width tolerance, roll length, core and joint policy apply to the sample?
- Which grade-specific compliance and technical files are available now?
- Can the sample be supplied in the proposed production format?
After the sample passes, review lot linkage, CoA release tests, retained records and change notification. This is more workable than sending a long audit form before a credible grade is identified.
FAQ
The exact code and construction, grade-specific ESD data and conditions, relevant thermal evidence, proposed roll specification and applicable documents. Record missing evidence as an open qualification item.
No. It describes charge dissipation under test conditions, not charge generated during unwind or removal. Qualify the actual event when it presents risk.
No. Evidence needs time, heating method, substrate, cycles and removal condition, followed by a representative process trial.
Agreed lot-specific release characteristics, results, limits and test identification. It must identify the supplied grade and lot rather than repeat typical TDS values.
Retain the approved roll and lot, define construction and roll specification in the purchase document, and require traceability and change notification. Compare a second lot for higher-risk programs.
No. Direct access may improve communication, but grade control, converting, traceability, documentation and contractual responsibility matter more than the word “factory.”
Request a Technical and Supplier Qualification Package
Send the substrate, masking position, thermal profile, ESD requirement, roll format, quantity and market. River Tape can identify a candidate construction and provide available grade-specific data. Final approval remains based on the customer’s trial and purchase specification.